Applications
Related Products


Benefits
Process
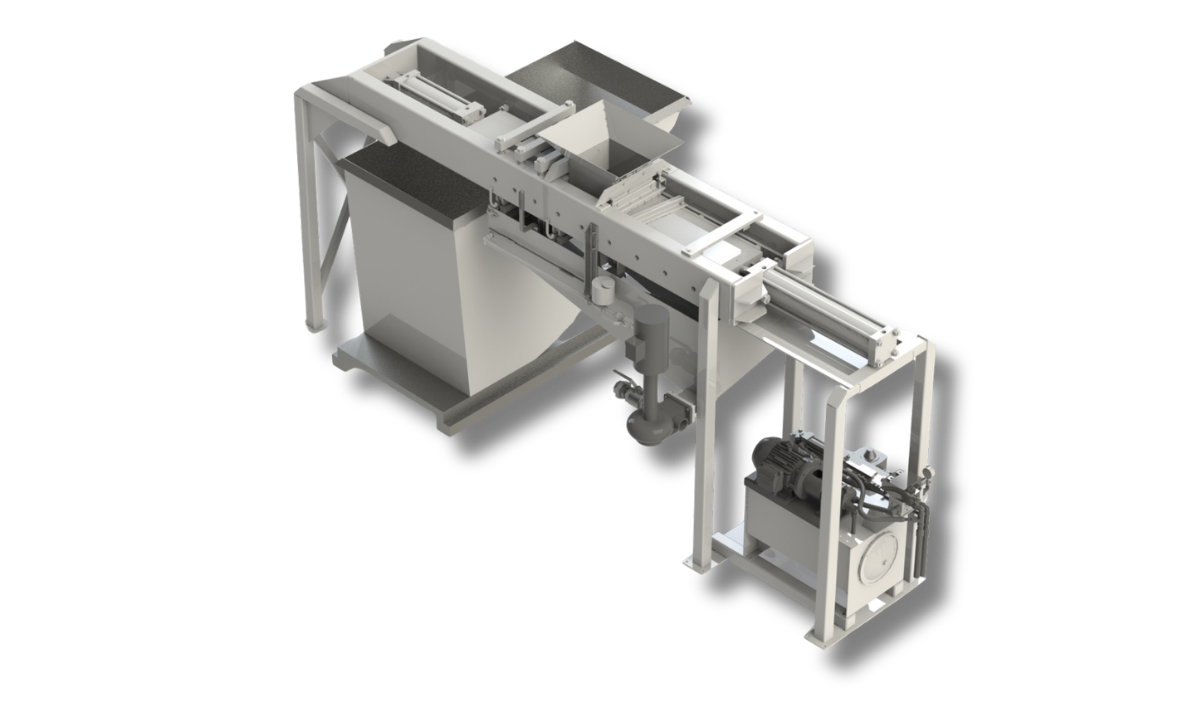
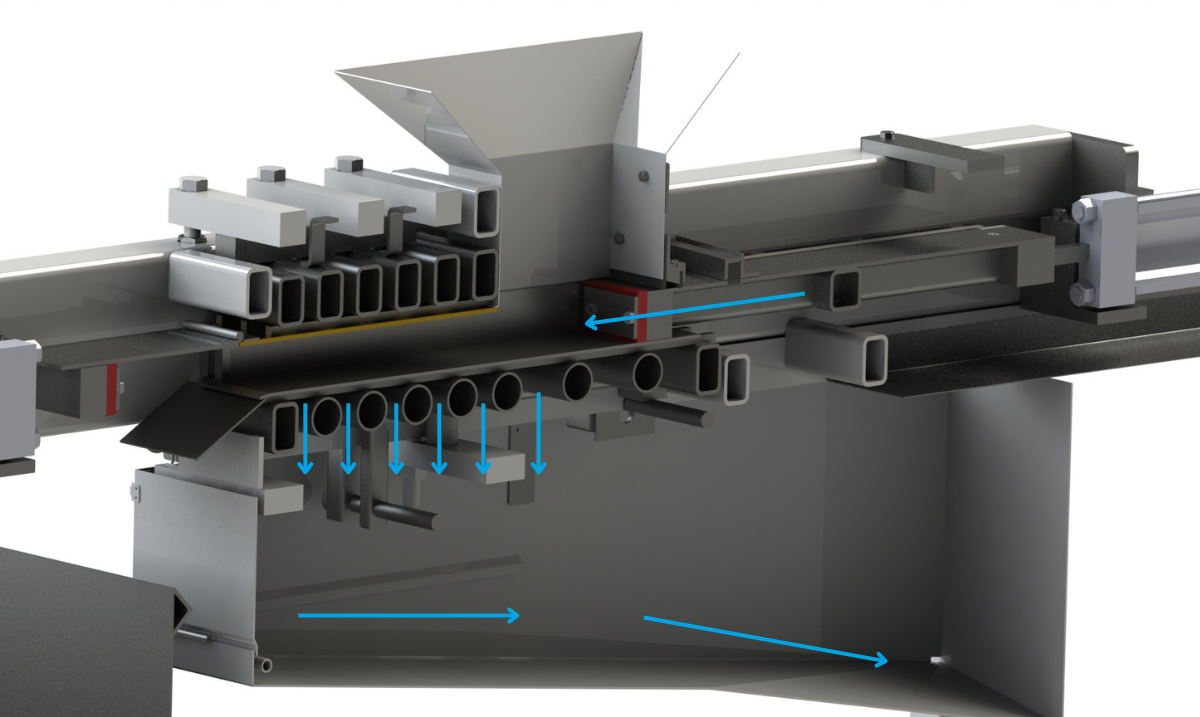
- Wet sludge enters the inlet chute from a feed conveyor or filter discharge.
- The system automatically detects sludge and initiates the compression cycle.
- The compression ram advances, pushing wet sludge into the compression chamber.
- The ram retracts to allow additional sludge into the chamber.
- Initial low-pressure compression allows free fluid to drain through the wedgewire screen.
- Compression pressure gradually increases to improve fluid removal.
- Once the cycle is complete, the plugging ram retracts to open the compression chamber.
- The compression ram advances to discharge the compacted sludge briquette.
System Benefits
- Automatic operation
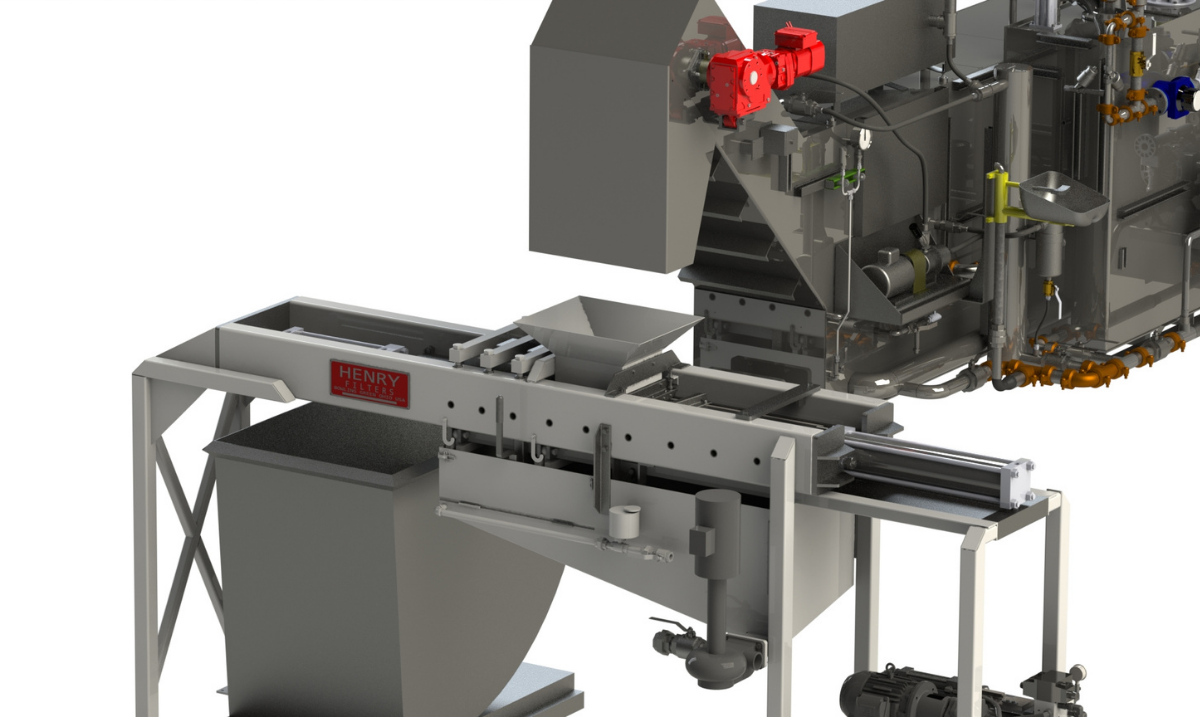
- Minimal floor space requirements
- Recovers valuable oil or coolant
- Produces dry, compacted sludge for transportation, recycling, or disposal
- Replaceable stainless steel de-liquefying screen panel
- Compact design allows installation beneath the filter discharge ramp
- Potential return on investment in less than one year through recovered fluids and reduced swarf disposal costs
- 2–16 cubic feet per hour (ft³/hr) - Based on application